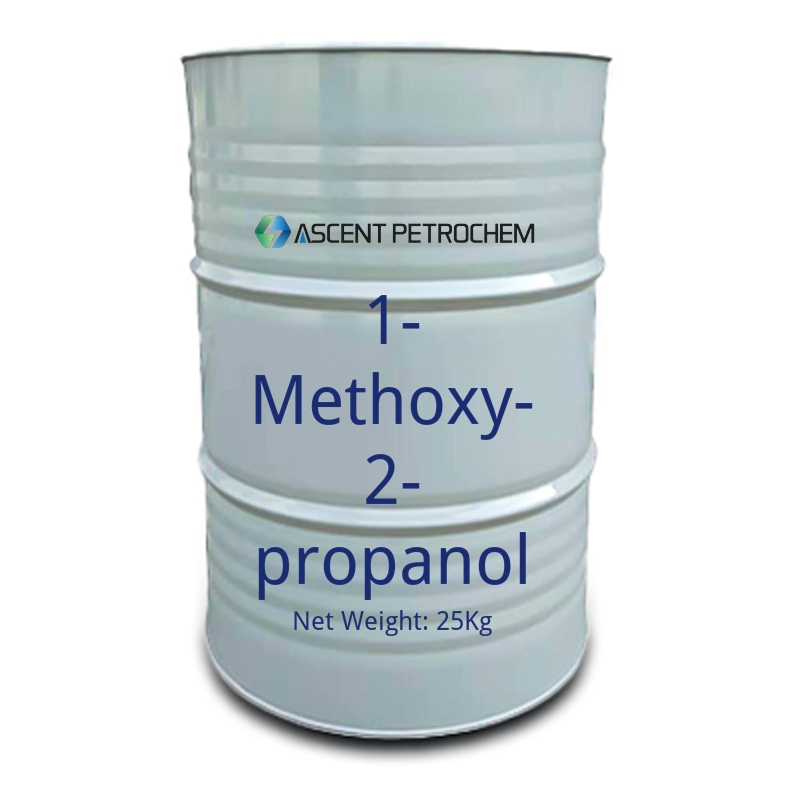
1-Methoxy-2-propanol
- Product Name: 1-Methoxy-2-propanol
- Factroy Site: Yudu County, Ganzhou, Jiangxi, China
- Price Inquiry: sales6@ascent-chem.com
- Manufacturer: Ascent Petrochem Holdings Co., Limited
- CONTACT NOW

- 1-Methoxy-2-propanol is typically used in formulations when viscosity and evaporation rate and flash point and VOC content must be controlled within specific ranges.
| HS Code | |
| Productname | 1-Methoxy-2-propanol |
| Chemicalformula | C4H10O2 |
| Casnumber | 107-98-2 |
| Ecnumber | 203-539-1 |
| Molecularweight | 90.12 g/mol |
| Appearance | Colorless liquid |
| Odor | Mild ether-like |
| Boilingpoint | 120 °C (248 °F) |
| Meltingpoint | -97 °C (-143 °F) |
| Density | 0.92 g/cm³ at 20 °C |
| Vaporpressure | 10.9 mmHg at 25 °C |
| Flashpoint | 32 °C (90 °F) closed cup |
| Autoignitiontemperature | 270 °C (518 °F) |
| Solubility | Miscible with water |
| Refractiveindex | 1.403 at 20 °C |
| Viscosity | 1.8 mPa·s at 20 °C |
| Logp | -0.49 |
As an accredited 1-Methoxy-2-propanol factory, we enforce strict quality protocols—every batch undergoes rigorous testing to ensure consistent efficacy and safety standards.
| Packing | 1-Methoxy-2-propanol is supplied in 200 L steel drums, 25 L HDPE jerricans, or 1 L glass bottles. |
| Container Loading (20′ FCL) | 20′ FCL container loading of 1-Methoxy-2-propanol in UN-approved drums, properly secured, labeled, and fully sealed for safe international chemical shipment. |
| Shipping | 1-Methoxy-2-propanol ships as UN 3092, Proper Shipping Name: 1-Methoxy-2-propanol, Hazard Class 3, Packing Group III. It is a flammable liquid requiring approved UN packaging, flammable-liquid labels, and compliance with ADR/IMDG/IATA rules. Keep away from heat, sparks, oxidizers, and open flames; use ventilation and grounding. |
| Storage | Store 1-Methoxy-2-propanol in a cool, dry, well-ventilated, fire-resistant area away from heat, sparks, open flames, and strong oxidizers. Keep containers tightly closed, properly labeled, and grounded. Use flammable-liquid cabinets with secondary containment. Protect from static discharge and incompatible materials. Store below 30°C, and keep spill kits and appropriate PPE available. |
| Shelf Life | Shelf life: stable under recommended storage; typically 24 months in sealed containers, cool, dry, away from heat and ignition sources. |
What Limits Coalescing Efficiency in High-Tg Acrylic Latex Films?
In waterborne acrylic and styrene-acrylic architectural and light-industrial coatings, 1-methoxy-2-propanol (PGME; CAS 107-98-2) is added as a coalescing solvent that lowers minimum film formation temperature (MFFT). The technical boundary is the solvent’s high water miscibility and its boiling point of 119–122°C at 101.3 kPa. In a direct-to-metal acrylic latex with an MFFT of 18–22°C as measured by ASTM D2354-10ε1, PGME at 5–9 wt% relative to binder solids typically depresses MFFT below 5°C. The coalescing action is governed by plasticization of the hard-phase polymer domains; PGME diffuses into the latex particle after water evaporation and reduces the glass transition temperature of the film during the early curing window. Because PGME is miscible with water and has a comparatively slow evaporation rate of 0.62–0.68 on the n-butyl acetate scale, a process conflict arises when formulation pH is maintained above 9.0 with an amino alcohol neutralizer. Under those conditions, PGME can be retained in the aqueous phase too long, producing open times beyond 120 s on vertical cold-rolled steel panels. Production-scale air-assisted spray equipment with reciprocating heads and a 200–250 μm wet-film deposition has shown that a flashed-off residence of 90–120 s at 20–25°C is required before forced curing at 60–70°C. The VOC content of the liquid coating is determined by ISO 11890-2:2020, and free glycol ether content is measured by ASTM D6886-14e1. Adhesion after 7-day ambient cure is evaluated by ASTM D3359-17; a 7 wt% PGME loading on binder solids with a 2:1 TiO₂-to-silicate extender ratio commonly gives a 5B classification on degreased cold-rolled steel. The terminal product is a waterborne direct-to-metal enamel for agricultural equipment frames with a 100 g/L VOC ceiling under South Coast Air Quality Management District Rule 1113; PGME is counted as a VOC and must be offset by reformulation or by acetone dilution. Corrosion resistance data for this exact configuration measured by ASTM B117-19 are limited in public literature, but scribe creep after 500 h is typically reported by additive suppliers in the 2–4 mm range when an organic-acid flash-rust inhibitor is present.
Semiconductor photolithography uses 1-methoxy-2-propanol as an edge-bead remover and resist thinner for positive-tone ArF and KrF chemistries. Electronic-grade material is specified for trace metals below 10 μg/L individual concentration and water below 0.1 wt%; these values vary by device node and photoresist supplier, and no single public SEMI document establishes a universal PGME specification. On a 300 mm coater/developer track, the solvent is dispensed at 0.8–1.2 mL/s onto the wafer edge while the chuck rotates at 900–1,500 rpm for 8–15 s. The surface tension of approximately 28 mN/m at 20°C provides wetting on low-k dielectric and silicon dioxide surfaces without down-set delamination. The boiling point of 119–122°C enables a post-rinse bake at 100–110°C to remove residual solvent before exposure; premature film collapse occurs if the bake ramp is faster than 1°C/s. The process window is narrow at the edge bead: a change of ±0.2 wt% in the PGME/ethyl 3-ethoxypropionate ratio shifts edge dissolution rate by more than 15%, producing either edge lift or bevel contamination on subsequent coating steps. Incompatibility arises with tetramethylammonium hydroxide developer if PGME residues above 5 μg/cm² remain on the wafer backside or bevel; such residues poison the developer bath and increase defect density. Acidity measured as acetic acid content above 50 mg/kg is a batch-control parameter because it correlates with post-exposure delay drift and linewidth roughness. The terminal use is a process fluid for logic and memory wafer patterning, not a standalone formulated product.
When PGME Replaces Ethylene Glycol Monoethyl Ether in Solvent-Based Flexographic Ink Blends
Flexographic and gravure packaging inks that once relied on ethylene glycol monoethyl ether have been reformulated with 1-methoxy-2-propanol to meet reproductive-toxicity restrictions. In nitrocellulose-based laminating inks for reverse printing on BOPP and PET, PGME is incorporated at 8–18 wt% of the liquid ink, with ethyl acetate at 35–45 wt% and n-propanol at 30–40 wt%. The slower evaporation rate of PGME, measured as 0.62–0.68 relative to n-butyl acetate, reduces early drying in the anilox cells of a 400–600 lines/cm flexographic plate. Ink viscosity is adjusted to 18–25 s in a DIN 4 flow cup at 25°C according to DIN 53211. On an eight-colour central impression press running at 200–250 m/min, PGME-containing blends reduce dot bridging by 10–15% compared with ethyl acetate/n-propanol-only controls. The solvent also dissolves polyamide and polyurethane resins at binder solids up to 25 wt% without causing gel particles on gravure cylinder chrome surfaces. Residual solvent in the printed laminate is measured by flame ionization detection gas chromatography following EN 13628-2; total residual solvent is commonly specified below 5 mg/m² before lamination. Food-contact compliance is established under Regulation (EC) No 1935/2004 and, for Swiss markets, the printing ink ordinance RS 817.023.21 Annex 2; PGME is listed, and the applicable specific migration limit must be verified against the current consolidated text. The terminal product is a flexible package for dry snacks and confectionery, with print-side lamination against a polyethylene or polypropylene sealant web.
When rosin flux residues must be removed from dense surface-mount assemblies, 1-methoxy-2-propanol functions as a semi-aqueous solvent in immersion cleaning baths. A typical bath operates at 45–55°C in a closed-loop agitated tank; the closed-cup flash point of 32°C imposes the upper bath-temperature limit when ventilation is interrupted. PGME is blended at 10–20 wt% with water and an alkanolamine at 2–5 wt% to maintain a pH of 9–11. The solvent reduces the surface tension of the bath to approximately 28–30 mN/m, which is critical for under-component penetration in assemblies with 0.5 mm standoff heights. Cleaning efficacy is evaluated by residual ionic contamination measured with a resistivity-solvent extractor per IPC-TM-650 2.3.25, with acceptance below 1.56 μg/cm² sodium chloride equivalent. The terminal product is a cleaned printed circuit board assembly prior to conformal coating. The main operational boundary is batch carry-out: without a two-stage deionized-water rinse at 40–50°C, PGME residues can remain in blind vias and soften acrylic conformal coatings.
Acid-Catalyzed Esterification to 1-Methoxy-2-Propyl Acetate
The conversion of 1-methoxy-2-propanol to 1-methoxy-2-propyl acetate (PGMEA) is a downstream derivative process that consumes large volumes of PGME. The esterification is conducted with acetic acid at a molar excess of 1.05–1.20 relative to PGME in a glass-lined jacketed reactor at 90–110°C. Sulfuric acid or a solid acid catalyst is used at 0.2–0.5 wt% of the reaction mass. Water formed during the reaction is removed by reactive distillation under reduced pressure, shifting equilibrium toward the ester. The crude ester is then neutralized, washed with aqueous alkali, and distilled to a final purity above 99.0 wt%. The process limitation is the formation of low-boiling azeotropes involving PGME, water, and acetic acid; published data for the exact composition at the process vacuum level are limited. The closed-cup flash point of 32°C and the boiling point of 119–122°C impose nitrogen inerting when the reactor liquid surface exceeds 60°C. The terminal product, PGMEA, has a boiling point of 145–146°C and is used in photoresist formulations. Purity and conversion are verified by gas chromatography against certified reference materials; residual acetic acid is maintained below 0.05 wt% to avoid downstream corrosion in semiconductor packaging applications. The process is operated under batch control with a reflux ratio above 3:1 during the distillation phase. The main incompatibility is with strong oxidizing agents and concentrated nitric acid, which can initiate runaway oxidation if the reactor jacket exceeds 150°C.
For agricultural emulsifiable concentrate and oil-in-water emulsion formulations, 1-methoxy-2-propanol is incorporated as a co-solvent and solubilizer for active ingredients with low water solubility. In a typical emulsifiable concentrate, PGME is used at 5–15 wt% of the total formulation, combined with aromatic hydrocarbon solvent and a nonionic/anionic emulsifier pair at 10–15 wt%. The role of PGME is to maintain a single liquid phase at 0°C and to prevent crystallization of the active ingredient during cold-dilution into hard water. Dilution stability is assessed using CIPAC MT 36.3; the emulsion must remain homogeneous without creaming or oil separation for 24 h at 30°C in water of 342 mg/L calcium carbonate hardness. The flash point of PGME contributes to the formulated EC flash point, which is measured by ASTM D93-20; many formulations fall below 35°C and require flammable-liquid storage. The terminal product is a field-crop herbicide or fungicide EC packaged in fluorinated HDPE containers. The operational boundary is the low-pH stability of the formulation: PGME is stable in the pH range 4–8, but prolonged storage at pH below 3 can lead to ether cleavage and formation of propylene glycol and methanol, which alters the cold-storage crystallization curve.
Automotive Refinish Basecoats Require Humidity-Tolerant Retarder Packages
Waterborne automotive refinish basecoats use PGME as a retarder and co-solvent to control drying in spray booths operating at relative humidity above 70%. In a two-component waterborne polyurethane system, PGME is added at 3–7 wt% of the ready-to-spray formulation, combined with deionized water and a polyurethane dispersion. The evaporation profile is designed to maintain an open time of 10–15 min at 23°C and 70–75% RH so that the basecoat levels before clearcoat application. Sag resistance is measured by ISO 16862:2006; formulations with 5 wt% PGME and a urethane rheology modifier at 1.2–1.8 wt% typically retain a sag limit above 175 μm wet film on vertical steel. Humidity-induced blushing is minimized because PGME has high water solubility and does not create a separate water-rich phase during the final flash. VOC content is measured by ISO 11890-2:2020; the added PGME is counted as VOC, so formulators cannot exceed the 250 g/L limit without using exempt acetone. The terminal product is a waterborne basecoat for collision repair shops, applied with HVLP spray guns at 1.4–1.7 bar air pressure. The main incompatibility is with high levels of acid catalyst in adjacent clearcoat layers; overspray contact can protonate the ether and accelerate solvent release, causing cratering. Published data on this specific interaction under collision-shop curing at 60°C for 30 min are limited.
Competitive 1-Methoxy-2-propanol prices that fit your budget—flexible terms and customized quotes for every order.
For samples, pricing, or more information, please contact us at +8618018036652 or mail to sales6@ascent-chem.com.
We will respond to you as soon as possible.
Tel: +8618018036652
Email: sales6@ascent-chem.com
Get Free Quote of Ascent Petrochem Holdings Co., Limited
Flexible payment, competitive price, premium service - Inquire now!
- 1-Methoxy-2-propanol is manufactured under an ISO 9001 quality system and complies with relevant regulatory requirements.
- COA, SDS/MSDS, and related certificates are available upon request. For certificate requests or inquiries, contact: sales6@ascent-chem.com.
Specification Profile and Purity Boundaries
Comparability between suppliers is established through a defined set of test methods. Gas chromatographic purity is usually reported as area percent by a supplier-specific GC-FID method calibrated with certified reference materials; no directly applicable ASTM purity standard exists for this particular glycol ether. Water content is measured by Karl Fischer titration according to ASTM E203, color is assessed against platinum-cobalt standards by ASTM D1209, density is measured by ASTM D4052 at 20 °C, and distillation range is determined by ASTM D1078 at 101.3 kPa. Acidity is expressed as acetic acid and measured by ASTM D1613.| Parameter | Typical specification | Test method |
|---|---|---|
| Assay as 1-methoxy-2-propanol | ≥ 99.5 % | Supplier GC-FID with certified reference material |
| 2-Methoxy-1-propanol | ≤ 0.3 % | Supplier GC-FID |
| Water | ≤ 0.10 wt% | ASTM E203 |
| Color | ≤ 10 Pt-Co | ASTM D1209 |
| Density at 20 °C | 0.916–0.921 g/cm³ | ASTM D4052 |
| Distillation range at 101.3 kPa | 118–122 °C | ASTM D1078 |
| Acidity as acetic acid | ≤ 0.01 wt% | ASTM D1613 |
How Does 1-Methoxy-2-Propanol Affect Minimum Film Formation Temperature in Waterborne Dispersions?
In thermoplastic styrene-acrylic and all-acrylic latexes, the solvent partitions between the aqueous phase and polymer particles; the coalescing effect depends on polymer glass transition temperature and hard monomer content. Differential scanning calorimetry of dried films indicates that addition of 3.0 wt% 1-methoxy-2-propanol depresses the minimum film formation temperature by 4 °C to 6 °C for a latex with a base MFFT of 18 °C, whereas 5.0 wt% can produce a depression of 7 °C to 9 °C when measured by the gradient bar method described in ISO 2115. The effect is not linear above 6.0 wt% because the solvent also increases ionic strength in the serum phase and reduces the swelling of alkali-swellable thickeners, producing a viscosity drop that must be corrected with associative polyurethane thickeners at 0.1 wt% to 0.3 wt% on total formula. On a 500-L pilot batch with a 4-blade impeller at 250 rpm, pre-dilution in the letdown water at a 1:5 solvent-to-water mass ratio prevented local polymer coagulation; direct addition at the same shaft speed generated gel particles larger than 50 μm when the batch temperature exceeded 30 °C. The solvent is therefore metered into the vortex at a feed rate not exceeding 0.5 L/min per 1000 L batch volume. Solventborne coil coatings rely on a narrow evaporation window between carrier evaporation and crosslinker activation. 1-Methoxy-2-propanol at 2.0 wt% to 4.0 wt% of total solvent increases sag resistance without raising viscosity above target when applied with a reverse roll coater at 60 m/min and peak metal temperature of 232–249 °C. In this window, the solvent must be removed before the melamine crosslinker reaches full activation; residual solvent above 0.05 wt% in the cured film can reduce methyl ethyl ketone double rubs by more than 50 % when tested by ASTM D5402. Thermogravimetric retention data from coil-coating lines show that the solvent is substantially released before the peak metal temperature, but published data for this specific configuration is limited to line-specific audits. In semiconductor resist processing, 1-methoxy-2-propanol is used as a diluent for photoresist thinning and edge-bead removal. Electronic-grade product specifications add chloride, nitrate, sulfate, and phosphate each below 0.1 ppm and metal cations below 0.05 ppm by inductively coupled plasma mass spectrometry. The material is filtered through 0.05 μm polytetrafluoroethylene membranes into fluoropolymer or high-density polyethylene containers under nitrogen. A 1:2 volume blend of 1-methoxy-2-propanol and propylene glycol monomethyl ether acetate is common in edge-bead removal because the blend shifts volatility between the two solvents; exact evaporation rate is determined by gas chromatographic headspace analysis under the coating tool exhaust conditions, and published data for this specific configuration is limited. Exhaust airflow in the coating bowl must remain above 0.4 m/s to prevent stagnation of flammable vapour, and ignition sources are excluded because the flash point of the neat solvent is 32 °C.When the α-Isomer Replaces Ethylene Glycol Monomethyl Ether in Printing Ink Diluents
Regulatory restrictions on ethylene glycol monomethyl ether, CAS 109-86-4, create a direct substitution case for 1-methoxy-2-propanol. EGME is classified as toxic to reproduction category 1B under CLP; the α-isomer does not carry the same reproductive toxicity classification, and industrial hygiene assessments typically use an 8-hour time-weighted average of 100 ppm and a short-term limit of 150 ppm for workplace exposure. In flexographic and gravure ink diluents, the substitution changes drying performance because 1-methoxy-2-propanol has a lower boiling point and a faster evaporation rate than EGME. On a six-colour central impression press running at 120 m/min with a 45 °C drying tunnel, press-side viscosity measured by DIN 53211 using a 4 mm flow cup increased from 22 s to 31 s over an 8-hour shift when the ambient temperature exceeded 28 °C; the use of press covers and a 0.5 wt% addition of dipropylene glycol methyl ether reduced the rise to 4 s. The ink formulation also requires a solubility re-check for nitrocellulose and polyurethane binders; 1-methoxy-2-propanol has a lower Hansen hydrogen-bonding parameter than EGME and may require a small addition of cyclohexanone to maintain resin dissolution in high-solids concentrates.Comparative Solvent Parameters for Replacement Decisions
| Parameter | 1-Methoxy-2-propanol | PGMEA | EGME |
|---|---|---|---|
| CAS registry number | 107-98-2 | 108-65-6 | 109-86-4 |
| Boiling range at 101.3 kPa | 118–122 °C | 145–147 °C | 124–126 °C |
| Closed-cup flash point | 32 °C | 43 °C | 39 °C |
| Water solubility at 20 °C | Miscible | Approximately 19 g/L | Miscible |
| Relative evaporation rate, n-butyl acetate = 1.0 | 0.62 | 0.33 | 0.5 |
| Key toxicological concern | Flammable liquid; no CLP reproductive toxicity classification | Flammable liquid; no CLP reproductive toxicity classification | Reproductive toxicity category 1B under CLP |